Every workstation has a story that unfolds slowly enough that nobody notices it…
Every workstation has a story that unfolds slowly enough that nobody notices it in real time. A technique drifts a few degrees off standard. A grip…
Every workstation has a story that unfolds slowly enough that nobody notices it in real time. A technique drifts a few degrees off standard. A grip…
If I could only monitor one thing in a plant, it would probably be the exits. Not because blocked egress is the most dramatic hazard. Because it is the…
Conciliar cuentas es una de esas tareas que consume horas de un equipo de finanzas revisando linea por linea, buscando la diferencia entre dos…
Your most dangerous moment is not a machine failure. It is week one for a new hire. They do not know the quirks. Which step is touchy, which guard…
Somebody told me last month that housekeeping is a supervisor problem, not a technology problem. He was right, and he was also describing exactly why…
A machine operator at a small parts machining shop mentioned to her supervisor, almost in passing, that her wrist had been bothering her for a while. A…
High utilization feels like success. Sometimes it is just expensive busyness. There is a deep instinct in operations to keep everything running. Idle…
¿En que paso exacto de su proceso revisa una persona lo que la IA generó? Muchas empresas adoptan una herramienta de IA y dejan esa pregunta sin…
In a furniture plant the housekeeping problem is not a mess. It is a gradient. Dust does not arrive. It accumulates, a little every shift, so there is…
Most safety systems are built to catch an event. A fall, a strike, a pinch point, something with a clear before and after that can be logged,…
The most common reason a good pilot never starts is that somebody assumed it needed a committee. It does not. It needs one person who owns the site and…
Ergonomics programs have always faced the same tradeoff: rigorous assessment takes time, and time is the one resource that limits how often any…
Revisar contratos consume horas de personas muy calificadas en tareas que no requieren todo su criterio: encontrar la cláusula de penalización,…
“All our operators are certified.” I believe you. Certification is also the single weakest predictor of how somebody drives on a Thursday in December…
The most dangerous container in your plant is the one everyone has stopped reading the label on. Chemicals become invisible through familiarity. The…
An auto parts assembly line had its ergonomic assessment scheduled, as usual, for a mid-week shift with normal volume. The assessor watched the…
La primera política de IA que necesita una empresa no es técnica. Es una lista: qué información sí puede usarse y cuál no. Sin esa lista, cada…
We are taught to see inventory as an asset. On a plant floor, big piles of it are usually a symptom of something wrong. Work in process stacked between…
A yard tractor backs a trailer toward a door. The driver checks his mirrors, sees nothing, and keeps coming. Somewhere behind the trailer, a man is…
En atención a clientes, la pregunta no es si la IA puede responder. Es quién responde por lo que dice. Un patrón que funciona bien con Claude es el de…
Ergonomics has good tools. The NIOSH Lifting Equation, RULA, REBA, and similar methods give a rigorous, well-validated read on the risk of a specific…
La protección de datos personales en México cambio de raíz este año, y muchas empresas todavía no se han dado cuenta. El INAI ya no existe. Desde marzo…
Thirty days into a Proactive Safety Intelligence deployment, the most common observation from plant leaders is not about the technology. It is about…
Every year around now, plants in cold climates start finding water inside the building, and every year it surprises somebody. It should not. The…
¿Su empresa ya quiere un piloto de IA, pero nadie ha definido para qué? Es la situación más común que vemos. El entusiasmo llega antes que la pregunta…
Your emergency plan is only as good as the last time you actually ran it. For a lot of plants, that was never. It is a binder. It has a flowchart,…
“We already painted the lines.” Almost everybody has. Yellow walkways, hatched no-go areas, crossing points, the works. It is one of the most common…
On day one of a new safety initiative at a cross-dock warehouse, a shift supervisor made his opinion known in the first team huddle: another program,…
Shopping for an AI safety platform feels a lot like buying a used car. Everyone’s brochure says “best in class.” Here is how to cut through it and what actually matters once the sales deck is closed. 7 questions to ask any vendor before you sign anything Does it work with the cameras you already…
There is a slump on your line, and it has a clock. Most plants just never look for it. Output is not flat across a shift. There is the slow start while…
A selector steps out from between two racks at the same moment a forklift comes around the end cap. The driver brakes, the selector jumps back, both of…
Ask what changes on a floor in the first month after a safety program upgrade, and most people picture new equipment: cameras going up, screens going…
Nuestro equipo ya es Certified en la Claude Partner Network. Nuestra gente cuenta con certificaciones de Claude, y seguimos construyendo a partir de…
Nuestro equipo ya es Certified en la Claude Partner Network. Nuestra gente cuenta con certificaciones de Claude, y seguimos construyendo a partir de…
Most plants already own the hardware for a better safety program. The cameras went up for loss prevention, access control or quality. And they ended up…
Every plant has a moment, once or twice a day, when the people who know what happened leave and the people who need to know arrive. That handoff is…
When a plant asks where to start, I almost never say “everywhere”. Three zones will tell you most of what you need to know. First, the dock. It has the…
Slips, trips, and falls sound boring right up until they are the reason someone is out for three months. They do not get respect because they are not…
A steel mill’s day shift dealt with a minor equipment issue two hours before shift change: a guard on a rolling line that had been temporarily removed…
If one person retiring or quitting would seriously hurt your operation, you do not have an expert. You have a single point of failure with a nice…
A permit is a promise about the future. It says who will go in, when, with what, and who will be standing by. Then the actual work happens, and reality…
On a curing press floor there is a rhythm. Presses open on a cycle, people move between rows on a cycle, and after a few months everybody’s timing gets…
If a plant tracked exactly when its incidents happened, not just which shift, a pattern would show up that most safety programs are not built to see. A…
People sometimes ask for a longer pilot, as if more time means a better decision. In my experience it means the opposite. A 90 day pilot has a built in…
Most incident prevention programs are built on top of whatever near misses got reported, which means they are built on a partial picture from the…
The most dangerous machine in your building probably is not on a production line. It is the forklift. We get used to them. They are everywhere, they…
A pulp and paper mill had the same near miss happen at least four times over two months, and not one of them was ever formally reported. An operator…
“Our incident rate is already low.” Sometimes that means you run a genuinely safe operation. Sometimes it means you have not had your bad year yet. The…
Two lines, same equipment, same product, same shift length. One outperforms the other by a wide margin, year after year. The machines are identical. So…
Nobody removes a machine guard out of carelessness. They remove it for a reason, and usually a good one. At a bakery, it was a divider that kept…
Ask any plant manager how many near misses happened last month, and the honest answer is almost always the same: fewer were logged than actually…
The fastest way to make a safety system useless is to draw the exclusion zones too big. I have seen a plant define the entire cell area as restricted,…
Most plants run two versions of the same floor. One lives in the safety report. One lives in the operations report. They rarely reference each other,…
If your safety plan leans heavily on PPE, you are defending the goal with no one else on the field. PPE is the last line of defense, by design. It is…
A beverage canning line had one changeover point that operations had flagged for months as the reason the line never hit its target run rate. Pallets…
Walk a cement plant with the safety manager and ask about any guard, any barrier, any painted line. Ask why it is there. A surprising number of the…
Safety teams and operations teams tend to look at a floor with different questions in mind, and rarely compare notes on where those questions lead….
Your scrap rate is a strategy. The only question is whether you chose it on purpose. Every plant has a number for how much material it throws away, and…
A part sticks in the mold. Clearing it the right way means stopping the cycle, waiting, opening up, reaching in. Clearing it the fast way means getting…
Ask most plants how confident they are in their safety program, and the answer usually comes with a caveat: confident during the hours someone is…
The single biggest reason plants put off safety monitoring is that they think it starts with a capital request. It does not. Walk your main aisle and…
Every plant has a report that gets produced every day, costs someone an hour to make, and is read by absolutely no one. It started for a reason….
“We tried a pilot like this. It went nowhere.” I get that one a lot and it is usually fair. When I ask what happened, the story is almost always the…
A chemical processing plant ran its safety audits like clockwork. Quarterly, thorough, well documented, always on a Tuesday. The plant also ran a…
The most dangerous words on a plant floor are not “watch this.” They are “we have always done it this way.” Every normalized risk started as a shortcut…
Lockout is not usually skipped on big jobs. Nobody rebuilds a drive without isolating it. Lockout gets skipped on the jobs that only take a second. A…
Most safety audits happen on a schedule that makes sense for the auditor and almost no sense for the hazard. Weekday mornings. Business hours. A…
Here is something most plants have never counted. Add up the hours of video your cameras record in a month. In a mid-size assembly plant with thirty…
Walk your plant on a Sunday when nothing is running, and listen. The stuff still humming, hissing, and glowing is your energy bill talking to you….
A sheet metal fabrication plant closed out the year with its best recordable rate in a decade. The safety board in the breakroom told a good story….
I have seen safety binders that could survive any inspection on earth sitting forty feet from a press with a guard interlock taped over. Both things…
The most chilling fact in safety: a large share of people who die in confined spaces are the would-be rescuers. Here is how it goes. Someone goes into…
Ask a plant manager when his floor is least supervised and he will tell you instantly. Usually it is a specific hour, on a specific shift, and he can…
Every safety program tracks a number that looks like progress and is actually a rearview mirror. The recordable incident log. It counts what already…
Week one of a pilot is loud. The system is new, the zones are freshly drawn, and your supervisors get more alerts than they want. That week is for…
Slow changeovers are one of the biggest hidden taxes in a plant, and most people just accept them as the cost of doing business. Every changeover is…
A steel service center doubled its internal audits last year. Twice the walks, twice the findings, twice the corrective actions closed out. The…
A mid-size injection molding plant spent four months evaluating a new camera and sensor package for its safety program. Vendor visits. A pilot area. A…
During washdown at a dairy plant, an operator’s foot goes out from under him on the ramp up to the tank platform. He catches the rail. He laughs,…
If your safety training ends with a signature and changes nothing on the floor, you did not train anyone. You generated a record. We have all sat…
Facilities already record more than security teams realize. Cameras that watch the loading dock. Cameras that watch a production line for quality….
When a multi-site operator asks about rolling this out to fourteen plants, my answer is always the same: let’s do one. Not because we cannot handle…
Safety leaders usually start this conversation with one question. What will it take to get ahead of the next incident? Operations leaders usually start…
Should you build your own plant-floor AI or buy it? Here is how I would think about it as an operator, not a vendor. Building feels appealing. It is…
“We don’t want to spy on our people.” Great. Neither do we. In fact, I prefer having this conversation on the first call rather than the fifth. The…
Here is a scenario that should feel familiar. Your audit binder is clean. Your incident rate is down from last year. Your supervisors are trained and…
Most safety programs are built to answer one question. What went wrong? That is a good question. It is just the wrong one to build a program around. By…
Everyone celebrates the go-live. Almost nobody checks what the thing looks like ninety days later, which is the only moment that actually tells you if…
People assume “safety AI” means a project. Consultants, a scoping phase, cameras on order, a go-live sometime after budget season. Here is what the…
The cheapest inspection in the world is still cheaper than the recall it prevents. People get this backwards. Inspection feels like cost. It is a line…
On a sort line, a jam is not an event. It is Tuesday. It happens six times a shift and the fix takes nine seconds: reach in, pull the thing out, belt…
Your recordable rate is a rear-view mirror. It is an honest, audited, extremely well-maintained rear-view mirror, and it tells you exactly nothing…
Every incident investigation I have ever read spends its time on the moment of impact. Almost none of them spend time on the four seconds before it. In…
The most dangerous machine guard is the one everyone has stopped seeing. Guards get removed for a quick fix and not put back. An interlock gets…
Let me tell you what Braingine does not do, because it saves everybody time. It does not read minds, so it will not tell you someone was about to make…
You have probably squeezed your machines for every point of efficiency. When did you last do the same for where your people stand? Labor allocation is…
A bottling plant I spoke with recently handles near-miss reporting the “right” way: real forms, polished presentations, and a monthly metric that gets…
Heat does not wait for your safety committee to meet. Every summer, in warehouses, foundries, kitchens, and any plant where the AC is a rumor, people…
A refrigeration contractor shows up at 6 in the morning to look at a chiller. He signs in at the gate, and then he walks the shortest route to the…
The most common way a safety system fails is not a bad detection. It is a correct alert that arrives somewhere nobody is looking. I have walked into…
“We already have a safety program.” I hear that a lot, and usually it is true. Written procedures, a trained committee, monthly walks, a real budget…
Most incident reports are written to close the incident, not to prevent the next one. You can tell by reading them. “Employee was not following…
A forklift backs out of a warehouse aisle at the exact second a picker steps around the rack corner with a stack of boxes blocking her view. Six…
A maintenance team that is always busy is not a good sign. It usually means they are losing. Run-to-failure feels normal because everyone is moving…
An operator takes a pallet jack diagonally across a pick aisle instead of going around through the marked lane. It saves him about eleven seconds. He…
I asked a plant manager last week what it would take to get real safety coverage on his floor without asking his EHS team to hire three more people. He…
Before you put AI on the plant floor, there are a few questions worth answering out loud, because if you do not, your team will answer them for you,…
A picker on a high-rack warehouse aisle bumps a box loose while reaching for the one behind it. It lands two feet from where another picker was…
Walk most plants and you will find your most experienced people spending half their day on things a machine should be doing. Counting. Checking….
A sewing line operator at a textile plant twists at the waist to reach a bin of finished pieces, hundreds of times a shift, for months. Nothing looks…
If your safety program is mostly about catching people doing it wrong, do not be surprised when people stop telling you anything. Punishment teaches…
A sawmill operator feeds a warped board into the saw at an angle he knows is not quite right, because stopping to reposition it slows the count….
The downtime that kills you is not the big breakdown. It is the hundred little stops nobody writes down. A jam cleared in thirty seconds. A changeover…
A contractor at a chemical plant pulls off his respirator early while still inside the containment area, just for a second, just to wipe his face….
The fastest way to make plant-floor cameras fail is to roll them out like surveillance. The moment people think a system is there to catch them, they…
Second shift at an automotive parts plant, a technician leans past the light curtain to clear a jam in the robotic weld cell without hitting the stop…
A near miss is just a hit that got lucky. Most plant floors are full of them. The forklift that came too close. The guard left open for ten minutes….
We schedule machines for maintenance. We schedule almost nothing for human fatigue, then act surprised when the 3 am shift has the accidents. Fatigue…
I get the same question on almost every first call with a distribution center: “how long is this going to take to stand up, and how long before we know…
Continuous improvement runs on data, and most plants are trying to improve using numbers nobody believes. You know the ritual. The report says one…
A sleeve catches on an unguarded conveyor roller on a packaging line. The operator pulls free before it becomes anything worse. The line lead writes it…
I sat in a cold storage facility last month reading a binder of quarterly safety audits going back three years. Every single one came back clean. The…
A press brake operator reaches into the pinch point to clear a jammed part instead of walking to the shutoff. It takes eight seconds longer to do it…
A forklift backs out of a warehouse aisle at the exact second a picker steps around the rack corner with a stack of boxes blocking her view. Six…
OEE is one of the most quoted and least understood numbers in a plant. People see a high availability number and relax. The machine is up, so we are…
A worker on a poultry cut line steps past the yellow floor line to grab a bin. Fifteen times a shift, nobody says a word about it. Here is the part…
A standard that nobody can see being followed is not a standard. It is a suggestion. Most plants have beautiful work instructions. Laminated, posted,…
When a defect reaches the customer, the instinct is to find who messed up. Usually that is the wrong question. If one tired operator on one shift can…
Your safety numbers might look great because they are quietly leaving people out. Contractors. Temps. The crew that comes in on the weekend to do the…
Before you buy a faster machine, find out if it will even help. I have seen plants drop serious money on a shiny new line, then watch total output…
If the main way you measure safety is counting injuries, you are driving by the rear-view mirror. Injury counts are lagging indicators. By the time the…
Unplanned downtime feels like bad luck. A bearing goes, a motor quits, a line stops. What can you do. A lot, actually. Most “sudden” failures were not…
Most lockout-tagout failures are not about the procedure. The procedure is fine. It is in a binder, signed, audited, perfect. The failure happens in…
The most dangerous near-miss is the one nobody reports. I saw it at a food plant a few months ago. An operator barely dodged a badly stacked pallet…
Quick quiz for plant managers: which OSHA standard covers ergonomics? Trick question. There isn’t one. OSHA pulled its ergonomics standard back in…
Retail is the most analyzed industry in the world — and the gap between the analytics on the corporate dashboard and what’s actually happening on the store floor has never been wider. Manual tracking, periodic audits, and store-level guesswork are the hidden tax on every chain. AI-powered operational intelligence finally closes that gap. The hidden…
Manufacturing floors are rich with sensors and starved of insight. The data is there — in cameras, PLCs, MES systems, and the heads of experienced operators. What’s missing is the layer that turns it into actionable intelligence in real time, without a multi-year integration project. That’s what AI-powered operational intelligence is finally delivering. The four…
Consumer Packaged Goods companies are operating distribution networks that span thousands of kilometers and millions of SKUs — and most of them are still doing it with manual tracking, point-in-time visibility, and reactive decision-making. The result: inefficient distribution, high logistics costs, limited product traceability, and inventory pain that compounds with every new product line. AI-powered…
Predictive Analytics: Using Computer Vision Data to Forecast Dock Activity When your dock starts predicting the future better than a fortune cookie, you know you’re doing something right! 🔮 Remember Magic 8 Balls? Give them a shake and hope for the best? That’s basically how most docks predict their workload. But what if your dock…
Employee Empowerment: How Dock Workers Benefit from Computer Vision Tools Turning your dock workers into superheroes – no radioactive spider bites required! 💪 Let’s address the elephant in the dock: “Will AI take our jobs?” Spoiler alert: Nope! It’s more like giving your team an Iron Man suit for logistics! 🦸♂️ Here’s what really happens…
Integration Success: Connecting Computer Vision with Your WMS and TMS Think your WMS and TMS can’t play nice with new tech? Hold my API! 🔌 Let’s talk system integration – you know, that thing that usually causes IT managers to mysteriously schedule vacation time! 😅 Common integration nightmares: “But our WMS is older than the…
ROI Deep Dive: The Financial Impact of Computer Vision in Dock Operations Warning: This ROI analysis contains numbers that may cause spontaneous happy dances in your finance department! 💰 Let’s talk money – not the “check is in the mail” kind, but the real “watch your dock transform into a profit center” kind! Remember when…
Weather-Proof Operations: How Computer Vision Adapts to Environmental Challenges Mother Nature throwing a tantrum? Our AI doesn’t need an umbrella to keep your dock running! 🌪️ Weather forecasts be like: “Sunny with a chance of complete chaos at your loading dock!” And somehow, that chance is always 100% during your busiest days. 🎯 Let’s talk…
Load Quality Assurance: Automated Inspection Systems for Perfect Shipments Your packages can’t ghost you anymore – our AI catches every imperfection before it becomes an ex-customer! 🔍 Let’s talk about load quality – you know, that thing your customers absolutely love to complain about on social media. “My box looked like it went twelve rounds…
Compliance Made Easy: Automated Documentation and Audit Trails Auditors showing up unannounced? Grab some coffee – we’ve got your paperwork covered! 📋✨ Let’s talk about everyone’s favorite topic: Documentation! watches logistics managers everywhere break into cold sweats 😅 Remember the last time auditors showed up and your team did the “Great Paper Chase of 2024”?…
Predictive Analytics: Using Computer Vision Data to Forecast Dock Activity When your dock data starts predicting the future, it’s not magic – it’s just really, really smart AI! 🔮 Remember when predicting dock traffic was about as accurate as forecasting the weather with a magic 8-ball? “Will we be busy tomorrow?” shake shake “Ask again…
Safety First: How Computer Vision Systems Prevent Dock Accidents and Injuries Here is the problem with most dock safety programs. They measure what already went wrong. The OSHA 300 log, the incident report, the after-action review – all of it is looking backward. Your workers deserve a program that sees what is about to go…
Beyond Barcodes: Using Computer Vision for Automated Package Identification Move over barcodes, there’s a new sheriff in town! 🔍 (And this one doesn’t need perfect lighting or yoga-level scanning positions) Let’s talk about barcodes – those zebra-looking stripes that dock workers have to scan like they’re playing Twister in the dark. 🎯 You know the…
Real-Time Load Validation: How Computer Vision Prevents Costly Shipping Errors Who needs a crystal ball when you’ve got AI eyes watching your shipments? Here’s how to predict (and prevent) costly mistakes before they happen! Remember that time you accidentally shipped a pallet of premium vodka to a kindergarten instead of the liquor store? Okay, maybe…
Computer Vision 101: Understanding the Basic Technology Transforming Shipping Docks Think your smartphone’s facial recognition is cool? Wait until you see what it can do for your dock! Remember when we thought automatic doors were high-tech? Those were simpler times. Today, I’m going to demystify computer vision in a way that won’t make your brain…
The Hidden Costs of Manual Dock Operations: Why Your Shipping Area Needs an Upgrade Your shipping dock is bleeding money faster than a shopaholic with a new credit card – here’s why Ever watched money literally walk out your dock doors? No, I’m not talking about theft – I’m talking about the silent profit-killer lurking…
The Silent Guardian: How AI Strengthens Retail Security You know what keeps retail executives up at night? No, it’s not the caffeinated break-room coffee – it’s shrinkage! But here’s a story that might make you smile… Last month at a store using Braingine, our AI spotted something curious: a customer who kept “forgetting” to scan…
From Retail Maze to Amazing: When AI Becomes Your Store’s Interior Designer! Ever watched a customer play an unintentional game of “Where’s Waldo?” with your product aisles? Or witnessed the classic “I just need milk but ended up in the garden section” phenomenon? Well, grab your virtual hard hat – we’re about to renovate retail!…
Visual Merchandising: The Science of Store Seduction Think visual merchandising is just about making things look pretty? Think again! At Braingine, we’ve discovered that every display tells a story – but not always the one you think you’re telling. Here’s a mind-bender: We recently analyzed a luxury retailer’s window display that looked absolutely stunning… and…
Meet Your Secret Shopper: AI With a PhD in People-Watching! Ever wonder what your store would say if it could talk? Well, thanks to Braingine, it’s not just talking – it’s spilling all the tea! Picture this: Last Tuesday, we discovered that Karen (not her real name, but you know the type) spent exactly 3.7…
The Future of Retail is Watching: Why Computer Vision is Your Next Strategic Investment Walking through a major retailer recently, I noticed something fascinating: customers picking up products, checking them, and putting them back – valuable behavioral data going completely uncaptured. This got me thinking about the untapped potential of computer vision in retail spaces.…
The Hidden Environmental Hero in Your Store: A Personal Journey with Smart Energy Management I’ll never forget the moment that changed how I think about retail energy usage. I was walking through a client’s store at closing time, watching the staff meticulously turn off lights and adjust thermostats zone by zone. That’s when it hit…
Preventing Cart Abandonment: The Power of Predictive Movement Analysis A revelation from our latest retail analysis at Braingine: 67% of cart abandonments show a distinct “frustration pattern” before they happen. It’s like watching a slow-motion replay of lost sales – but what if we could change the ending? Let me share a story that changed…
Weather-Smart Retail: How AI is Turning Weather Patterns into Profit Patterns Just had a fascinating conversation with a store manager who couldn’t figure out why their staffing was always off on rainy days. That’s when I shared something that blew their mind: weather patterns don’t just affect what customers buy – they fundamentally change how…
An eye-opening stat crossed my desk this morning: retailers lose an estimated $3.7 billion annually due to poor display compliance. But here’s what really got my attention – 42% of promotional displays are not executed according to plan. Let me share a recent transformation story:A major retail chain was struggling with brand partnership revenues. Their…
The Hidden Killer of Retail Profits: Understanding the True Cost of Out-of-Stocks A shocking reality that still affects retailers: the average retailer loses 4% of their annual sales to out-of-stocks. But here’s what keeps me up at night – that number only tells part of the story. Let’s dive into the real impact: The immediate…
Real-time Planogram Optimization: When Your Shelves Learn from Your Customers Let me share something that changed my perspective on retail layouts forever. Last week, I watched a customer pick up a product, walk halfway down an aisle, return it, and choose something else instead. Traditional retail would call this indecision – at Braingine, we call…
Are you aware of the Real Risk of Identity Theft because of Privacy violations?
There is a lot of concern about the use of Biometrics in relation to citizen Privacy, we analyze if the use of Biometrics is or isn’t a violation of Privacy.
Even now, after years of biometric identification has been in place, there are huge users’ concerns about biometric misuse and privacy invasions, the reasons remain poorly articulated and the user fear remains high.
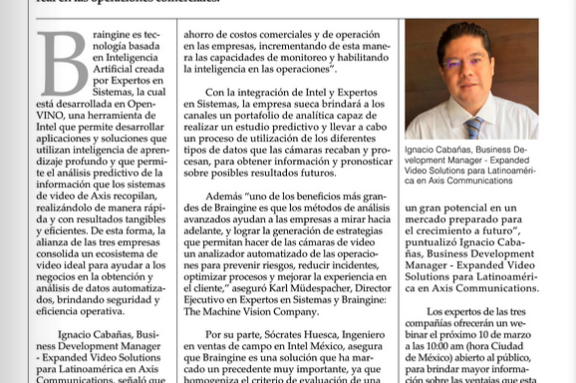
Axis Communications en conjunto con Intel y Expertos en Sistemas, introducen Braingine Crear un mundo más inteligente y seguro ha sido el punto de partida para la constante innovación tecnológica de Axis Communications, y en su afán por seguir brindando al mercado soluciones de vanguardia, han acordado una alianza estratégica con Intel y la compañía…
It was a Saturday evening and it was about to get dark when as a 7 year old boy I arrived a home but this time it was different, I was coming from the Boy Scouts and this time I walked back home alone, since my parents had taken my brother and little sister with…
WHAT DO WE NEED TO DO NOW? As AI becomes an ever more central part of every aspect of people’s lives, people should be able to trust it. Trustworthiness is a responsibility for every company and professionist that is pushing and promoting AI, and not just to find out use cases with the sole objective…
Industrial Safety is a top priority since it saves human lives and avoids physical damage, however it is an outstanding and daily challenge for basically all industries, there is plenty research on the subject that helps us understand how we can increase prevention effectiveness. As a start, and like Peter Drucker said “if you can’t measure…
We use essential cookies to run this blog, and self-hosted visitor statistics to understand which articles are read. Those statistics stay on our own server and are not shared with an advertising or analytics provider. We do not use cookies to personalize content or to advertise to you. By clicking Accept, you consent to the non-essential cookies. See our Privacy Policy.